Discover how THT Supply delivered high-performance valve solutions and integrated logistics to ensure project success and operational excellence.
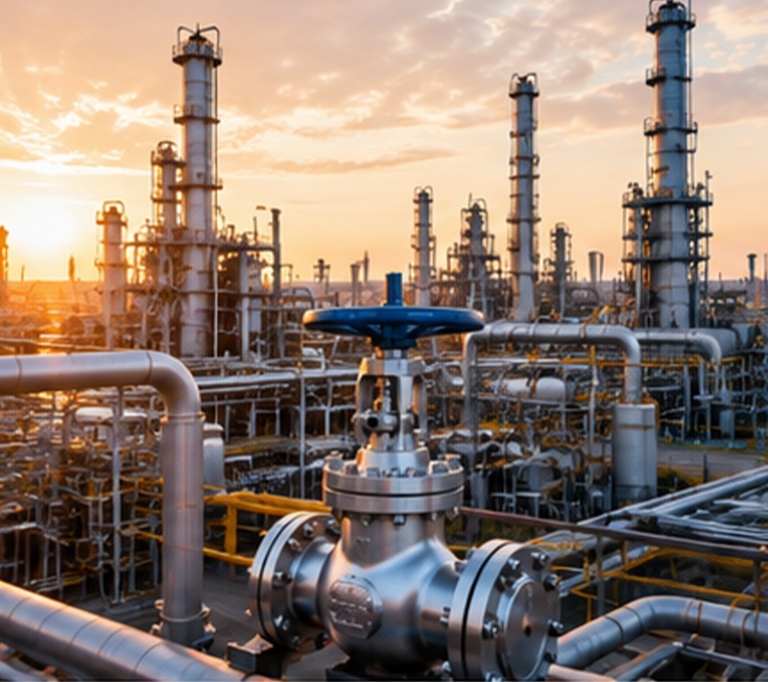
A large petrochemical and refining complex adopted our industrial valve solutions across crude oil distillation, catalytic cracking, delayed coking, and sulfur recovery units. These processes require valves capable of handling high temperatures, high pressures, and corrosive media.
The project utilized API 600 gate valves, globe valves, swing check valves, trunnion-mounted ball valves, and metal-seated ball valves for process isolation, flow control, and equipment protection. With excellent sealing performance and long service life, the valves help reduce emissions, improve operational safety, and ensure continuous production in critical refining operations.